Threads are one of the most common fastening features in mechanical design and CNC machining. They are widely used in mechanical assemblies, fastening applications, pipe sealing, and power transmission systems. Selecting the appropriate thread type, profile, pitch, and standard not only affects component compatibility but also has a direct impact on machining difficulty, assembly reliability, and service life.
This guide covers the most common thread types, metric and imperial thread standards, the differences between coarse and fine threads, tap drill sizes, and 2D drawing callout conventions to help engineers select the right thread specification, reduce design errors, and improve manufacturability.
CNC Maching Common Thread Types
Thread Types by Profile
1. ISO Metric Thread (M, 60°)
Available in coarse and fine pitches, ISO metric threads are the standard choice for fastening applications such as bolts and nuts.
2. Whitworth Thread (W, 55°)
A traditional British thread form commonly found on older British machinery and legacy equipment.
3. Pipe Threads (For Pipe Sealing)
• G – 55° Parallel Pipe Thread (BSPP, non-pressure sealing)
• R / Rp / Rc – 55° Tapered Pipe Thread (BSPT, pressure-tight sealing)
• NPT / NPTF – 60° American Taper Pipe Thread
4. Trapezoidal Thread (Tr, 30°)
Used for power transmission applications, including lead screws, lifting mechanisms, and adjustment screws.
5. Buttress Thread (B, 3°/30°)
Designed for heavy axial loads in one direction, commonly used in jacks, presses, and lifting equipment.
6. Square Thread
Provides the highest transmission efficiency but offers poor centering ability and wears relatively quickly. Typically found on older vises and lifting screws.
7. Round Thread (Rd)
Features a rounded profile that is resistant to dirt and damage, making it suitable for lamp sockets, hose couplings, and similar applications.
Thread Standards
1. Metric Thread (M)
Measured in millimeters and widely used in ISO, GB, DIN, and other metric standards.
2. Unified Thread (UN/UNC/UNF)
Imperial thread system used primarily in North America.
• UNC – Unified National Coarse
• UNF – Unified National Fine
3. British Standard Whitworth (BSW/BSF)
Traditional British thread standard used on legacy equipment.
4. Pipe Thread Series (G, R, NPT)
Designed specifically for fluid and gas piping systems.
Coarse vs. Fine Threads: What's the Difference?
Key Characteristics
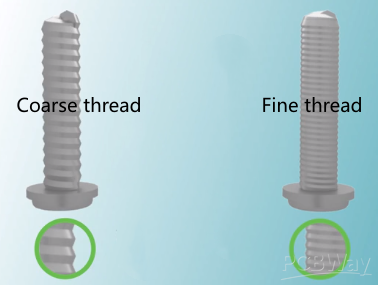
Coarse threads have a larger pitch and deeper thread profile. The pitch is omitted by default in thread callouts (e.g., M10). They are easy to manufacture and assemble, compatible with most standard fasteners, and are commonly used for general-purpose fastening. However, their larger helix angle provides lower self-locking performance than fine threads.
Fine threads have a smaller pitch and must always include the pitch in the thread designation (e.g., M10 × 1.0). They offer better self-locking performance and are commonly used in thin-walled parts, hydraulic fittings, precision components, and applications requiring higher vibration resistance or fine adjustment.
Strength Comparison
Coarse threads generally provide better resistance to damage during assembly, while fine threads offer slightly higher tensile strength and improved sealing performance.
For threaded fasteners of the same strength grade, preload capacity is similar. However, fine threads provide better resistance to loosening under vibration when no additional locking method is used.
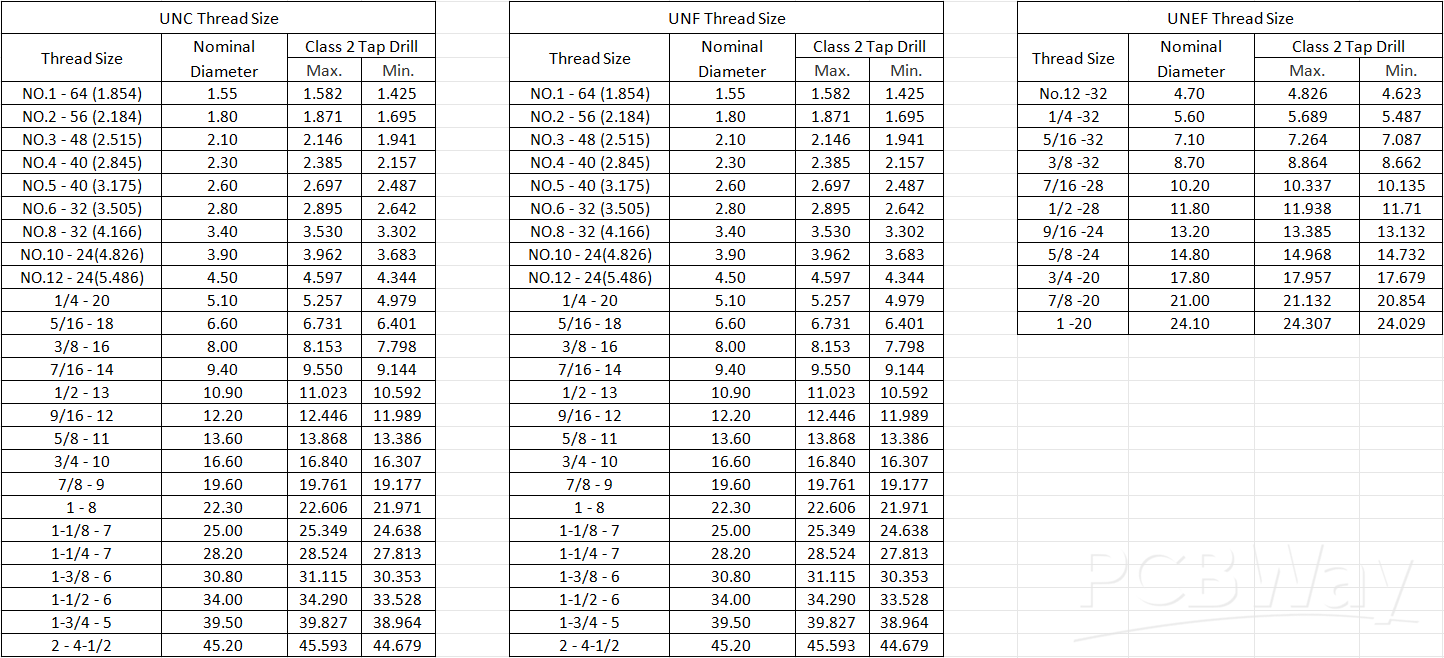
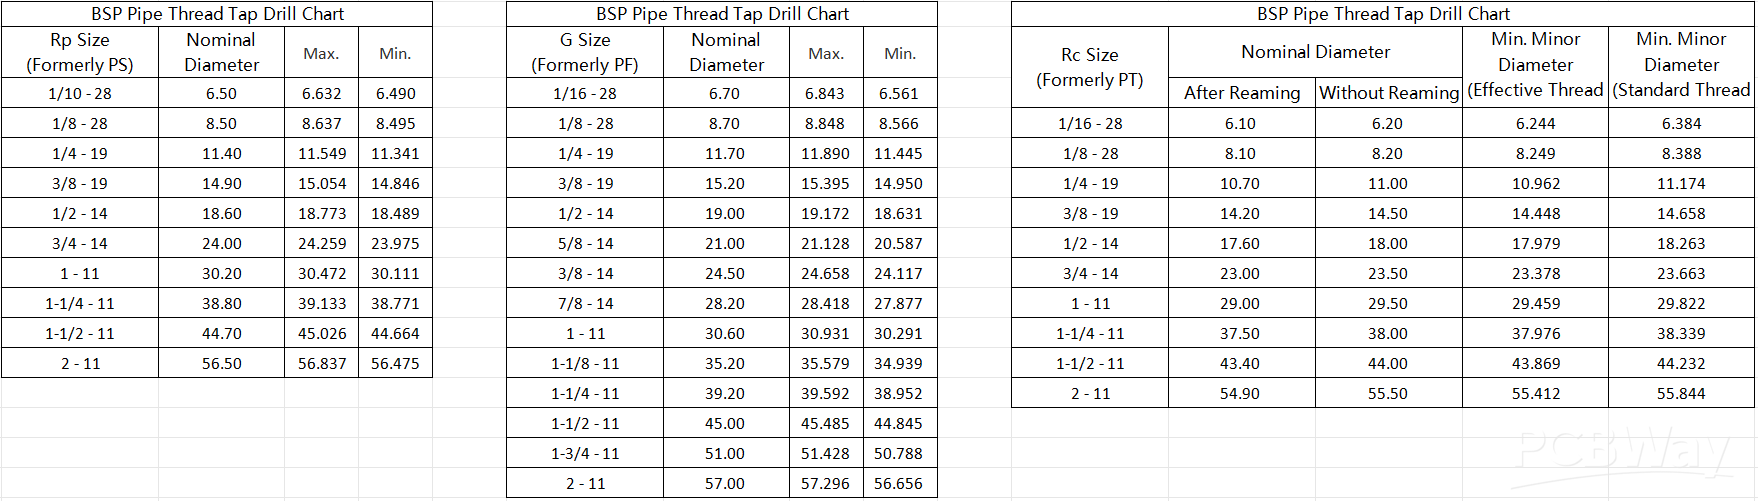
Thread Tap Drill Size Standards Chart
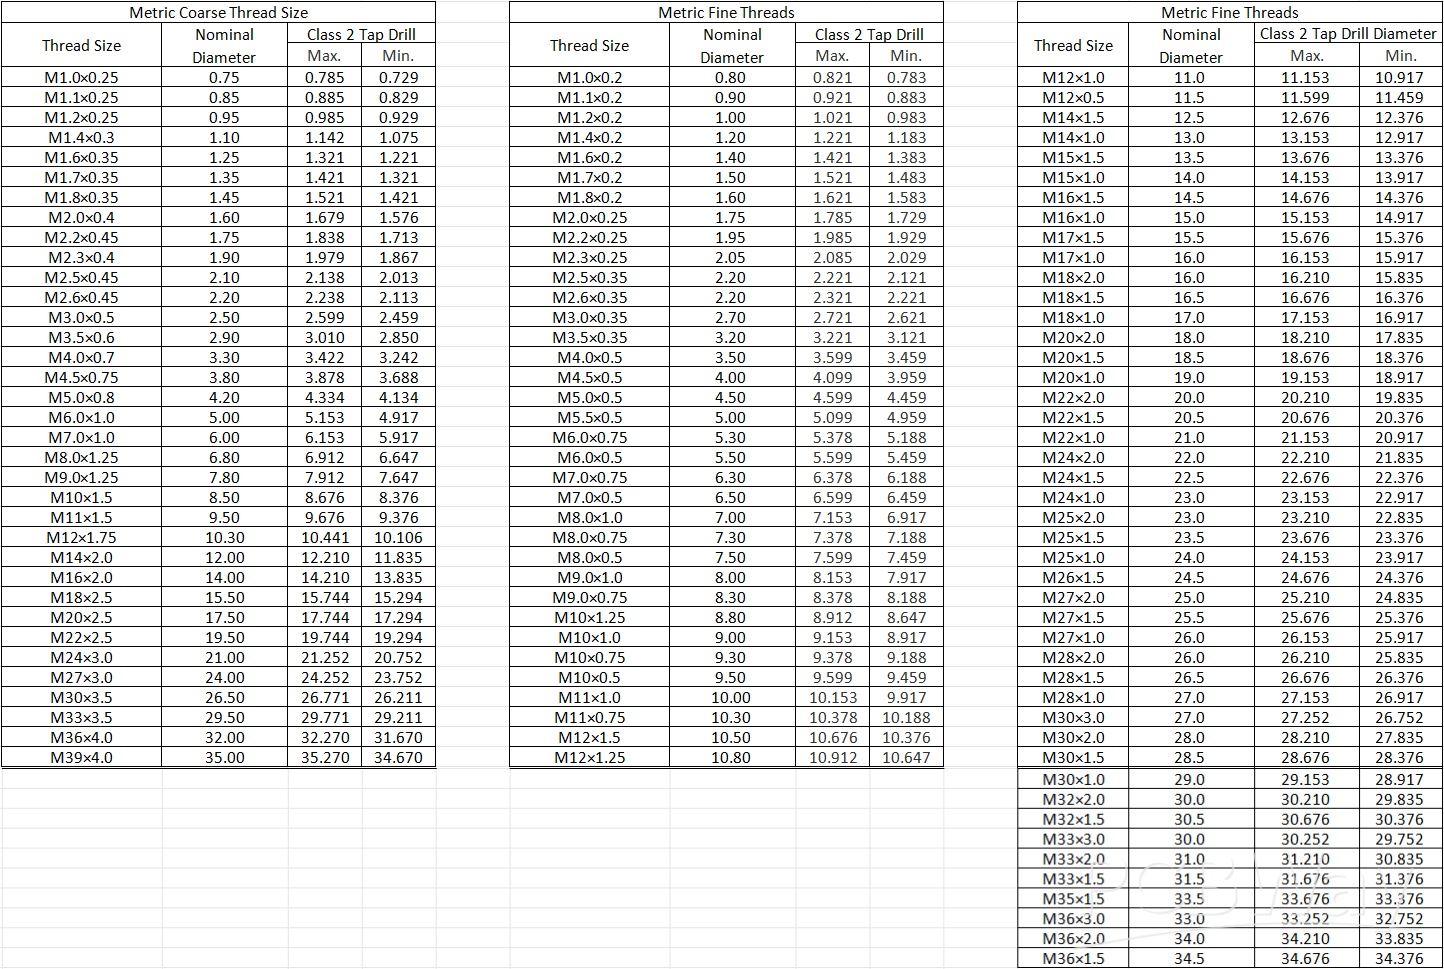
Before tapping an internal thread, the correct tap drill hole must be prepared. The tap drill diameter directly affects thread quality. If the tap drill hole is too large, the resulting thread profile will be incomplete, reducing thread height and engagement area. This lowers the load-carrying capacity of the thread and may lead to thread stripping. If the tap drill diameter approaches or exceeds the thread's major diameter, the tap cannot generate a complete thread profile, resulting in an unusable thread. For this reason, tap drill sizes should always follow the recommended tap drill charts.
For ductile materials (steel, brass, copper, aluminum alloys), material is plastically displaced during tapping: Tap Drill Diameter = Major Diameter − Pitch (d = D − P)
For brittle materials (such as cast iron, cast bronze, and hard plastics): Tap Drill Diameter = Major Diameter − 1.05 × Pitch (d = D − 1.05P)
Example: M10 × 1.5 (Metric Coarse Thread), Ductile materials: 10 − 1.5 = 8.5 mm; Brittle materials: 10 − (1.05 × 1.5) = 8.425 mm.
Metric Thread Tap Drill Chart
Unified Thread Tap Drill Chart
British Pipe Thread Tap Drill Chart
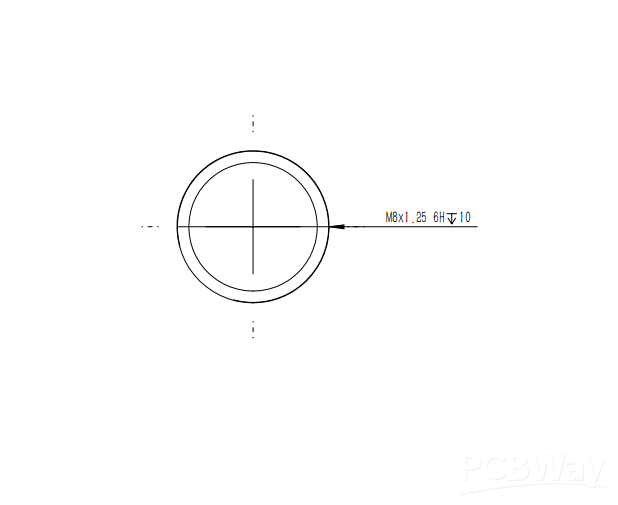
2D Drawing Thread Callout Standards
1. ISO Metric Threads
Format: M Major Diameter × Pitch – Tolerance Class – Hand – Engagement Length
Example: M10 × 1.5 – 6H – LH – S
• M – Metric thread designation
• 10 – Nominal diameter (mm)
• 1.5 – Pitch (omit for coarse threads)
• 6H – Internal thread tolerance class (6g for external threads)
• LH – Left-hand thread (right-hand is default)
• S – Short thread engagement (N = Normal, L = Long)
2. Unified Threads (UNC/UNF/UNEF)
Format: Nominal Diameter – Threads Per Inch – Series – Class – Hand
Example: 1/4-20 UNC-2B-LH
• 1/4 – Nominal diameter (inch)
• 20 – Threads per inch (TPI)
• UNC / UNF / UNEF – Thread series
• 2B – Internal thread class
• 2A – External thread class
• LH – Left-hand thread
3. BSP Parallel Pipe Threads (G/PF)
Format: G Nominal Pipe Size – Tolerance Class – Hand
Example: G 1/2-A-LH
• G – BSP parallel pipe thread
• 1/2 – Nominal pipe size (inch)
• A – External thread tolerance class
• Internal threads do not specify a tolerance class.
• LH – Left-hand thread
4. BSP Taper Pipe Threads (Rc/Rp/R)
Format: Thread Designation Nominal Pipe Size – Hand
Example: Rc 1/2-LH
• Rc – Internal taper thread
• Rp – Internal parallel thread
• R – External taper thread
• 1/2 – Nominal pipe size
• LH – Left-hand thread
For pressure-tight pipe threads, pitch, tolerance class, and engagement length are defined by the applicable standard and therefore are not included in the drawing callout.
Thread Callout Placement
1. Callout Location
• Threaded holes: Place the callout adjacent to the dimension or on a leader pointing to the thread axis.
• External threads: Attach the callout to the shaft dimension or use a leader pointing to the major diameter.
• Blind holes: Specify both the thread depth and drill depth.
Example: M6 × 1.0 × 10 / 12 (10 mm is the effective thread depth and 12 mm is the drill depth.)
2. Conventional Thread Representation
External threads: Major diameter shown with a thick continuous line; minor diameter with a thin continuous line.
Internal threads (section view): Major diameter shown with a thin line; minor diameter with a thick line.
Simplified representation: The tap drill diameter and depth may be indicated using the diameter symbol (Ø), followed by the thread specification.
Notes:
⒈ Coarse metric threads may omit the pitch (e.g., M10), while fine threads must specify the pitch (e.g., M10 × 1.0).
⒉ Standard tolerance classes include 6H/6g for metric threads and 2A/2B for Unified threads.
⒊ Only left-hand threads require the LH designation.
⒋ Blind holes should always specify both effective thread depth and drill depth.
⒌ Engineering drawings may reference applicable standards such as GB/T 197-2018 or ISO 965-1.
CNC Thread Design Guidelines
Proper thread design not only improves assembly reliability but also reduces machining costs and the risk of manufacturing defects. When designing threaded features for CNC machining, consider the following recommendations:
• Choose standard thread sizes whenever possible. Standard metric, unified, and pipe threads are easier to machine, inspect, and source.
• Avoid excessively deep threaded holes. Deep threads increase machining time and the risk of tap breakage. A thread engagement length of 1–1.5 × the nominal diameter is sufficient for most materials.
• Provide adequate bottom clearance for blind holes. Leave extra drill depth below the threaded section to accommodate the tap chamfer and ensure full thread engagement.
• Select the appropriate thread type for the application. Coarse threads are recommended for general fastening, while fine threads are better suited for thin-walled parts, vibration-prone assemblies, or precision adjustments.
• Specify complete thread information on engineering drawings. Include the thread standard, size, pitch (if applicable), tolerance class, thread depth, and handedness when required.
• Consider material machinability. Soft materials such as aluminum are generally better suited to coarse threads, while fine threads are more appropriate for applications requiring higher strength or positioning accuracy.
How to Choose the Right Thread
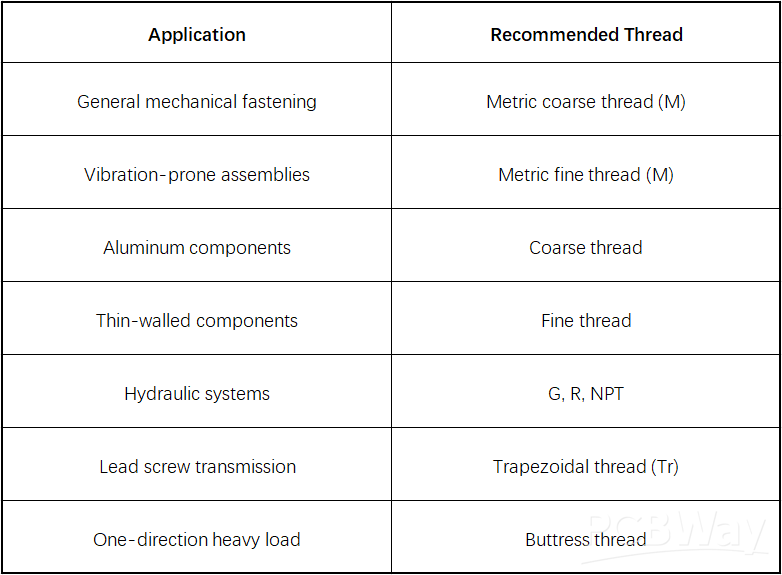
Unless a specific application requires otherwise, metric coarse threads are the preferred choice for general mechanical design because they offer the best compatibility, lowest machining cost, and widest availability of standard fasteners.
Selecting the appropriate thread type, tap drill size, and drawing callout not only improves assembly reliability but also reduces CNC machining complexity and manufacturing costs. For deep threads, small thread sizes, or high-precision threaded features, considering machining limitations during the design stage can effectively reduce the risk of tap breakage, insufficient thread strength, and other common manufacturing issues.
If your project requires parts with internal or external threads, PCBWay offers a one-stop CNC machining service, from design review and DFM analysis to precision manufacturing. We support metric, unified, pipe, and custom thread machining, helping you produce high-quality threaded parts that meet your drawing specifications with accuracy and reliability.