What Is an R Corner?
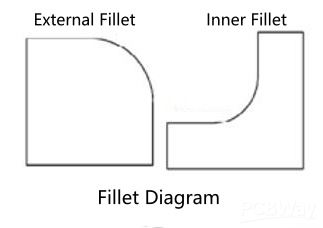
In CNC milling, an R corner (corner radius) refers to the rounded internal or external corner created by a rotating milling cutter. Since end mills are cylindrical cutting tools, they cannot machine a perfectly sharp internal corner. Instead, the cutter naturally leaves a radius that matches its cutting path.
For internal corners, the minimum achievable radius is determined by the cutter radius. A perfectly sharp inside corner is impossible with conventional CNC milling. External corners, however, can be machined with virtually any specified radius because the cutting tool can approach the edge freely.
The corner radius is one of the most fundamental geometric features in CNC machining and plays an important role in manufacturability, machining efficiency, and part strength.
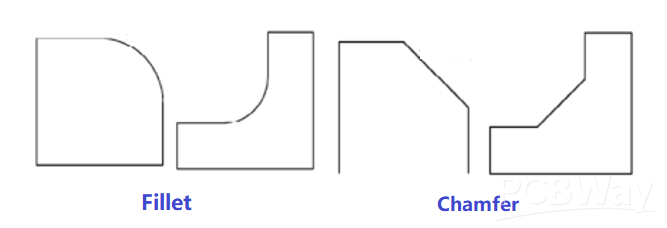
Fillet vs. Chamfer: Which One Should You Choose?
Although both fillets and chamfers eliminate sharp edges, they serve different engineering purposes.
Choose a Fillet (R Corner) When:
• The corner is part of the load path and experiences bending, torsion, or cyclic loading.
• Improving fatigue resistance is important, such as at shaft shoulders, bracket transitions, or gear roots.
• Fluid passages require smooth transitions to reduce turbulence.
• A continuous curved appearance is desired, such as for consumer electronics housings.
Choose a Chamfer When:
• The primary purpose is deburring or providing an assembly lead-in, such as hole entrances or thread starts.
• The external edge only needs to remove sharpness without reducing stress concentration.
• The goal is the lowest machining cost and shortest cycle time.
• A precise locating surface is required during assembly.
Design Tip:
For non-structural pocket corners, allowing the standard corner radius produced by a conventional end mill—or using a simple chamfer—is usually sufficient. Reserve fillets for locations where stress reduction or fatigue performance is critical.
Two Types of R Corners in CNC Machining
1. Internal R Corner
An internal R corner is the rounded corner found inside pockets, cavities, slots, or stepped features. It is naturally produced by the rotating end mill during machining.
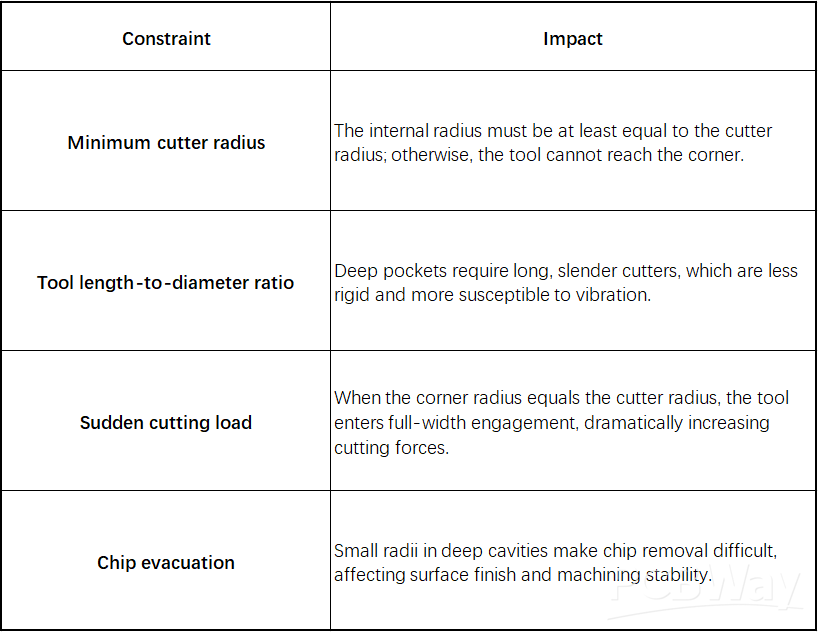
To ensure stable cutting, the internal corner radius should be slightly larger than the cutter radius, with 130% of the cutter radius widely regarded as a practical design guideline.
For example, when using a 10 mm diameter end mill (5 mm radius), the internal corner should ideally be R6 or larger. This provides a smoother toolpath, reduces chatter, minimizes tool wear, and improves dimensional accuracy.
2. External R Corner
External R corners are much less constrained than internal ones because the cutting tool can freely approach the outside edge of the workpiece.
Common machining methods include:
• Corner rounding cutters
• Ball nose end mills for 3-axis contour machining
• Standard 2D contour milling operations
As a result, external corner radii offer much greater design flexibility and generally have a much smaller impact on machining cost than internal radii.
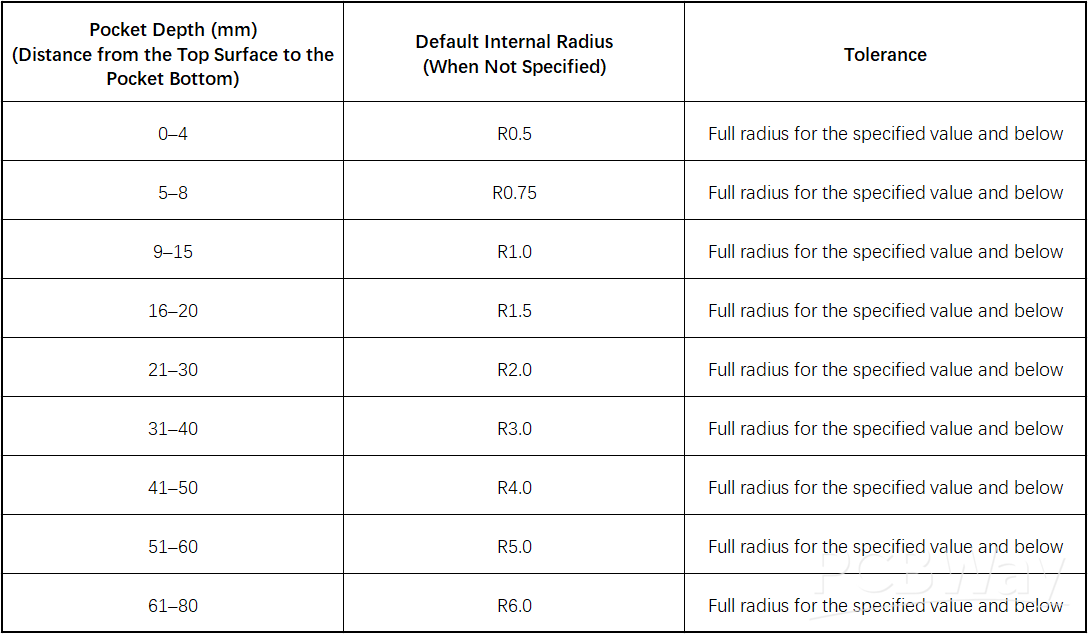
Default Internal Corner Radius Standards
Unless otherwise specified on the drawing, CNC machining typically follows standard internal corner radius recommendations based on pocket depth and material type. Selecting an appropriate standard radius helps improve machining efficiency, reduce tooling costs, and ensure stable cutting performance.
Standard Internal Radius for Aluminum Alloys and Non-Metallic Materials
Standard Internal Radius for Steel, Stainless Steel, Brass, and Copper
Applicable materials include: Carbon steel, Tool steel, Mold steel, Spring steel, Stainless steel, Brass, Copper.
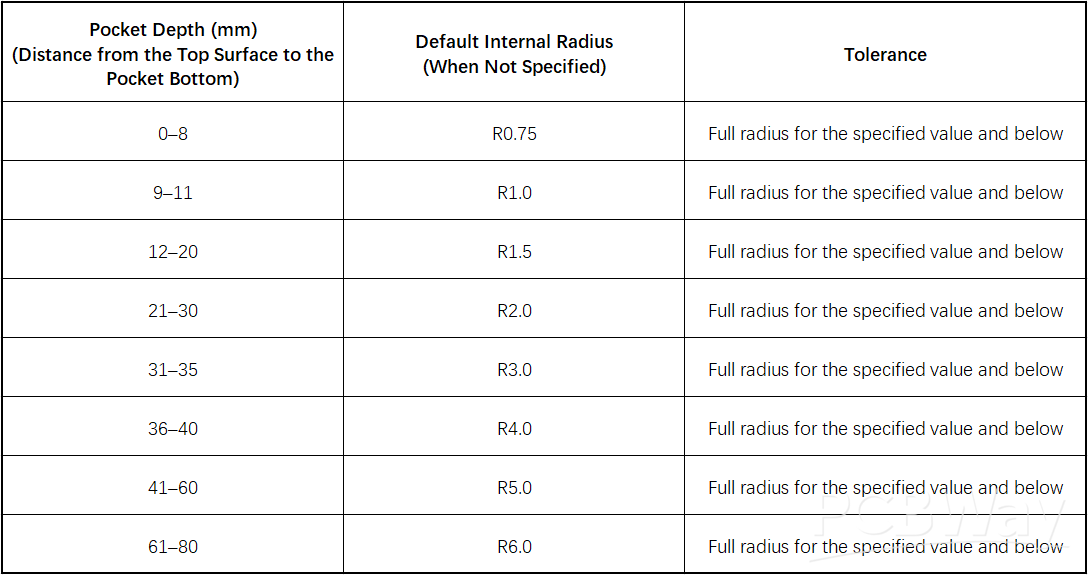
Note: These values represent recommended manufacturing defaults when no specific corner radius is defined on the engineering drawing. Functional or assembly-critical features should always follow the design requirements.
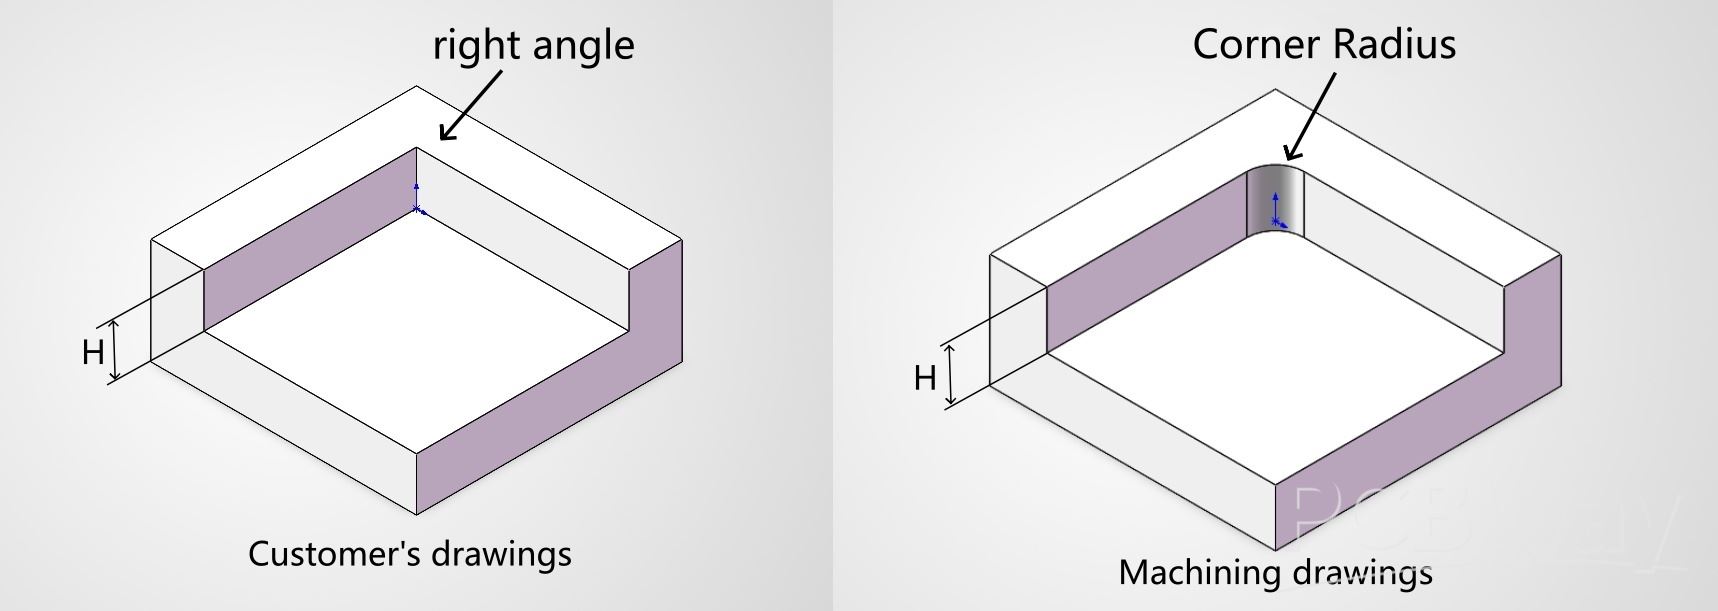
CNC Corner Radius Design Guidelines
Choosing an appropriate corner radius is one of the simplest ways to improve machining efficiency while reducing manufacturing costs. The following design rules are widely accepted in CNC machining.
Rule 1: Radius Should Be at Least One-Third of Pocket Depth
For internal pockets and cavities, the corner radius should ideally be at least one-third of the pocket depth.
Using a larger cutter improves rigidity, allows higher feed rates, and significantly extends tool life.
Example:
For a pocket with a depth of 12 mm, the recommended internal radius is R4 or larger. This allows the use of an 8 mm diameter or larger end mill, resulting in faster machining, better surface finish, and improved dimensional accuracy.
Rule 2: Internal Radius Should Be Larger Than the Cutter Radius
The internal corner radius should always be greater than the cutter radius. A practical recommendation is the 130% Rule, where: Internal Radius ≥ 1.3 × Cutter Radius.
Reason:
• When R = the cutter radius, the cutter enters full-width engagement at the corner, causing a sudden increase in cutting load.
• This can lead to tool chatter, poor surface finish, reduced dimensional accuracy, and accelerated tool wear.
Rule 3: Standardize Non-Critical Corner Radii
For non-functional features, use the same corner radius throughout the entire part whenever possible.
Standardizing corner radii offers several advantages:
• Fewer tool changes
• Shorter setup time
• Simpler CAM programming
• Lower risk of programming errors
• Reduced tooling inventory
• Lower overall manufacturing cost
In production environments, limiting a product family to three or four standard corner radii can reduce CAM programming time by 20–30% while improving manufacturing consistency.
Material Considerations for Corner Radius Design
Different materials have unique machining characteristics, requiring different strategies for selecting internal corner radii.
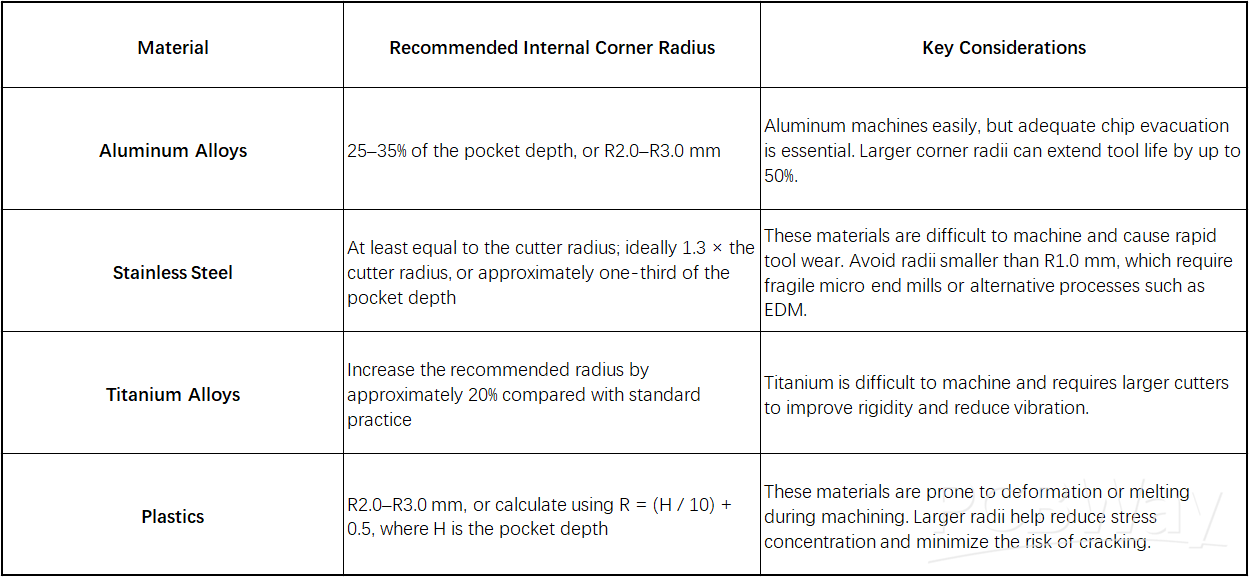
Note: For 316L stainless steel or hardened steel, machining an internal radius smaller than R0.5 mm typically requires a ball nose end mill with a diameter of 1 mm or less. These cutters are fragile, wear quickly, and significantly reduce machining efficiency. If a nearly sharp internal corner is functionally required, consider Electrical Discharge Machining (EDM) instead.
Corner Radius and CNC Machining Cost
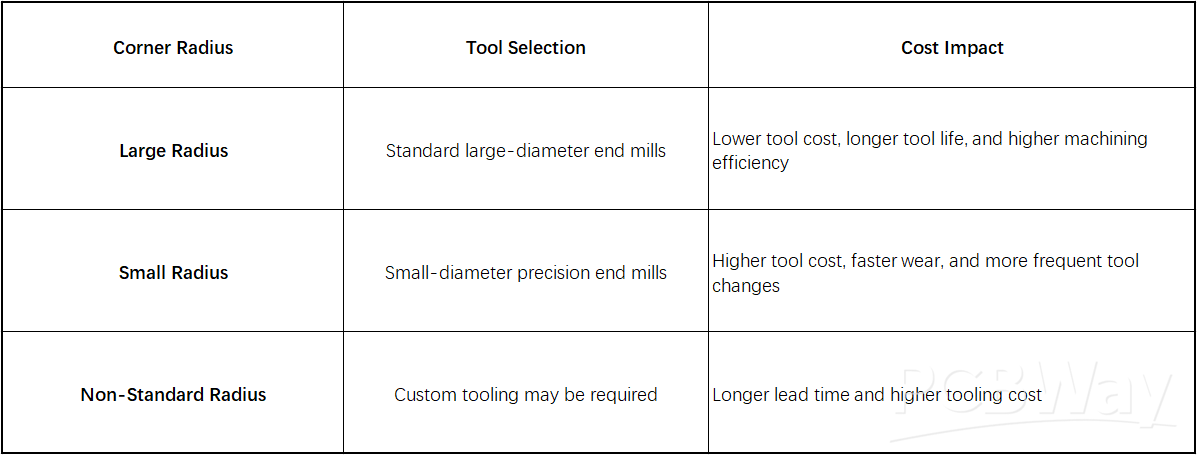
In CNC milling, the cost impact of a corner radius is determined primarily by tool selection, machining efficiency, and manufacturing process, rather than by the amount of material removed.
Although an R0.5 corner removes slightly less material than an R3 corner, it usually requires a much smaller cutter, lower cutting parameters, and additional finishing passes. As a result, the overall machining cost is often higher, not lower.
Tooling Cost
Machining Time
Increasing an internal corner radius from R0.5 to R3 can typically reduce machining time by more than 30% because:
• Larger end mills provide greater rigidity and support higher feed rates.
• Larger cutters require fewer toolpaths to machine corners.
• Small cutters must run at lower cutting parameters and often require multiple finishing passes to achieve the required dimensional accuracy and surface finish.
• Slower tool wear reduces tool changes, further shortening the overall machining cycle.
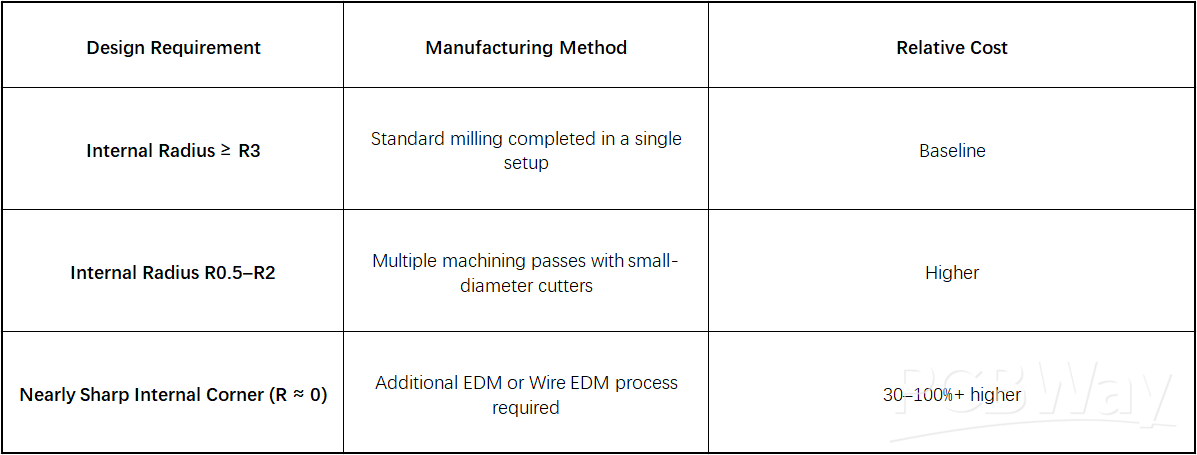
Manufacturing Complexity
Conclusion
Optimizing corner radius design early in the product development process can significantly improve manufacturability, shorten machining time, extend tool life, and reduce production costs.
Whether you need DFM analysis, precision CNC machining, or surface finishing, PCBWay provides a one-stop CNC manufacturing solution to help transform your designs into high-quality machined parts with greater efficiency and lower overall cost.